


Ball Screw Whirling Machine
Designed for high-efficiency thread machining of long-shaft components such as ball screws and worm shafts, the high-precision CNC ball screw whirling machine is a dedicated solution for precision transmission manufacturing. Using high-speed whirling cutter head enveloping milling, threads are formed in a single pass, achieving high productivity with minimal grinding allowance and making the system well suited for batch production environments.
Widely adopted in the precision machining of ball screws, planetary roller screws, and large-lead transmission screws, this whirling system serves as a core piece of equipment for the mass production of precision transmission components.
| Model | ||||
| Max. Installation Diameter | Ø160mm | Ø160mm | Ø160mm | |
| Max. Processing Length | 3000mm | 4000mm | 6000mm | |
| Max. Processing Diameter | Ø80mm | Ø120mm | Ø120mm | |
| Min. Processing Diameter | Ø16mm | Ø20mm | Ø20mm | |
| Rotation Speed of Workpiece | 0-20rpm | 0-20rpm | 0-20rpm | |
| Processing Speed | 500-2000rpm | 500-2000rpm | 500-2000rpm | |
| X-Axis Stroke | +100rpm, -30rpm | +100rpm, -30rpm | +100rpm, -30rpm | |
| Helix Angle | ±20° | ±20° | ±20° | |
| Number of Thread Starts | 1-24 | 1-24 | 1-24 | |
| Processing Accuracy | Within 2π Radians, ≤ | 0.007mm | 0.008mm | 0.008mm |
| Within Any 300mm, ≤ | 0.016mm | 0.023mm | 0.023mm | |
| Surface Roughness | Ra≤0.4μm | Ra≤0.4μm | Ra≤0.4μm | |
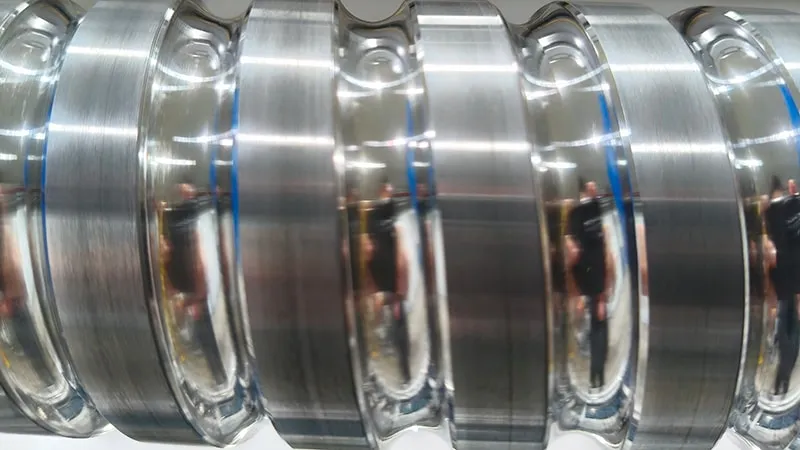
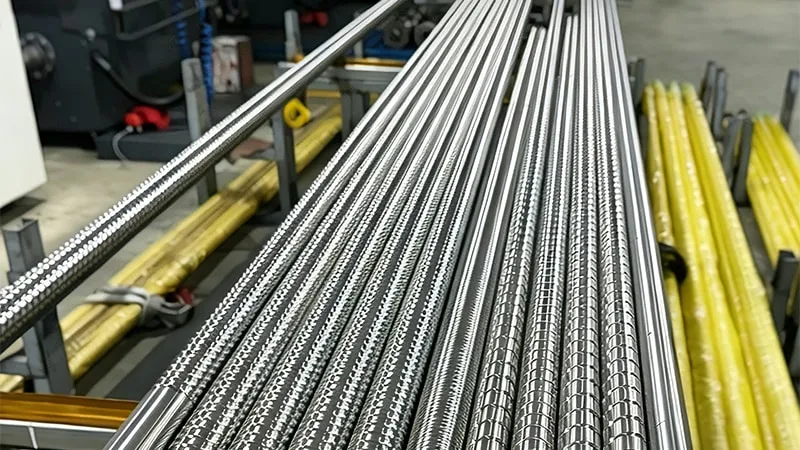
- Workpiece: Ball Screw Shaft
- Material: GCr15
- Workpiece Diameter: Ø80 mm
- Thread Lead: 30 mm
- Thread Starts: 1-start
- Surface Roughness: Ra 0.8μm
- Grinding Allowance: 0.25 mm
- Tooling: PCBN Whirling Insert
- Machining Process: Semi-Finishing Whirling
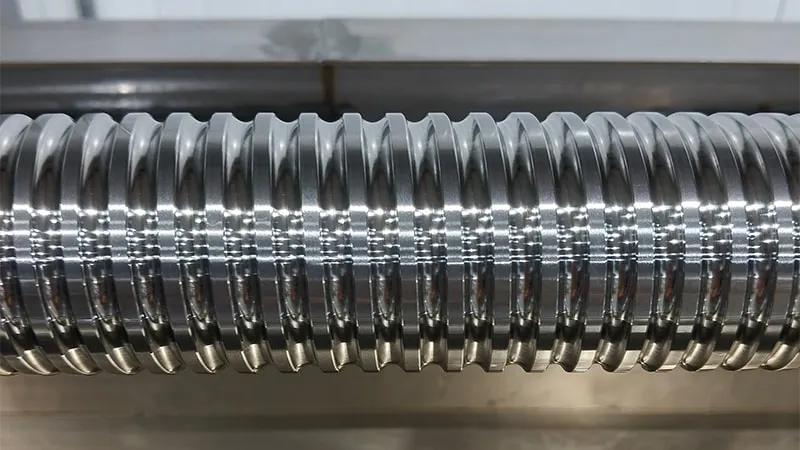
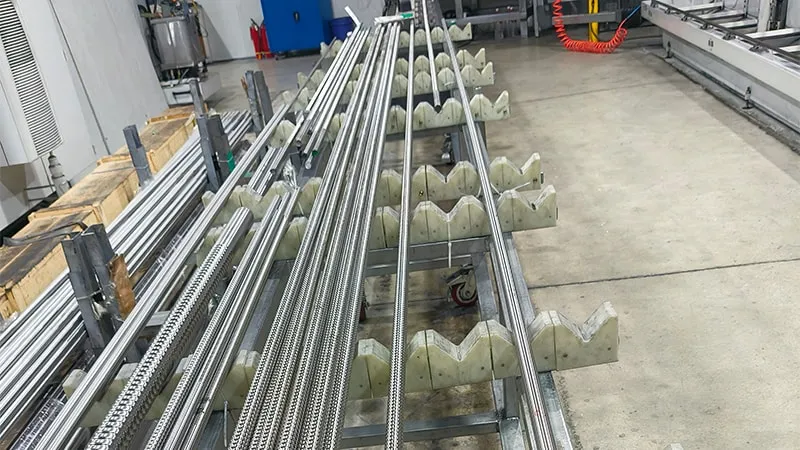
- Workpiece: Ball Screw Shaft
- Material: 50CrMo4
- Workpiece Diameter: Ø25 mm
- Thread Lead: 10 mm
- Thread Starts: 1-start
- Machining Process: Semi-Finishing
- Surface Roughness: Ra 0.5μm
- Grinding Allowance: 0.2 mm
- Tooling: PCBN Whirling Insert
For long-shaft ball screw production, thread whirling streamlines machining processes and minimizes thermal and stability problems typically encountered with conventional turning and grinding.
| Conventional Machining | Thread Whirling |
| Turning and grinding require multiple machining steps and longer processing time | Roughing and semi-finishing are completed in a single whirling setup, improving machining efficiency |
| Grinding requires substantial grinding fluid and generates grinding waste | Supports dry cutting or minimum quantity lubrication (MQL), reducing reliance on large volumes of cutting fluid |
| Higher thermal input can increase the risk of grinding burn, microcracking, and white-layer formation | Lower thermal impact, with much of the cutting heat carried away by the chips, reducing heat-related surface damage |
| Long, slender workpieces are more susceptible to deformation during machining | Optimized cutting-force direction improves machining stability, making the process well suited to batch production of long ball screw shafts |
- Easy Operation: The control system is equipped with SIEMENS 828D/840D CNC platforms, combined with HEIDENHAIN/FAGOR precision linear scales and Renishaw encoders, enabling full closed-loop control.
- Intelligent Compensation: Features single-pass cyclic milling with automated capabilities for continuous machining, multi-start thread milling, dynamic tool setting, and precise lead/pitch diameter taper compensation.
- Stable Precision: Synchronous CNC control guarantees superior lead accuracy and profile consistency. Precisely controlled grinding allowances fully support C3/C5 grade ball screw process chains.
- High Flexibility: By changing the cutter head and adjusting the A-axis, complex thread forms such as multi-start threads, variable-lead threads, and planetary roller screws can be processed with ease.
- Green Machining: Supports dry cutting and minimum quantity lubrication (MQL), significantly reducing coolant consumption and environmental disposal costs.
- High Machining Efficiency: Roughing and semi-finishing can be completed in a single setup, significantly shortening machining time—by 5 to 10 times compared with conventional turning. This process is suitable for batch production of long ball screw shafts.
- Durable PCBN Tooling: Equipped with Winice's self-developed custom PCBN whirling inserts. The wear-resistant cutting edges reduce tool-change frequency and setup time. The inserts can be reground and reused 3–5 times, lowering overall tooling costs.